Copyright © 2020-2021 Shenzhen CDTech Electronics LTD. All rights reserved. Site Map Powered by iwonder.cn

display / touch / bonding solutions
display / touch / bonding solutions
A display that has turned yellow in the field is usually reported as a screen discoloration and blamed on the panel. By the time the report reaches engineering, the evidence is often a phone photograph taken under unknown lighting, with no test pattern, no temperature and no record of how the unit was mounted. The useful question is not whether the colour looks wrong but which layer changed and under what conditions. This guide sets out the observation order, the pattern tests that separate source content from the optical stack, the role of temperature and assembly pressure, and the measurement record that makes a discoloration RMA actionable.
Record pattern, position, geometry and history first.
Start with the test pattern, affected area, viewing angle, panel temperature and time in service, because each narrows the cause before any instrument is used.
The first record should describe what was on the screen and where the colour changed. A tint that covers the whole panel points to the backlight, the polarizer or a global setting. A patch that follows a corner or an edge points to assembly pressure, edge seal damage or a local bonding defect. A band that moves with the viewing angle points to the optical stack rather than the source. Write the position in panel coordinates and photograph it with a scale, so the same region can be re-measured later.
Add the conditions: ambient light, panel brightness setting, warm-up time, panel temperature and the time the unit has been in service. A cold panel can show a colour shift that disappears after ten minutes, and a panel that has run for thousands of hours may have aged differently from a new sample. Without these fields, two observations that look contradictory may simply describe different states.
Test patterns separate source content from the panel.
If a tint appears only in photographs it may be source or profile; a neutral full-field pattern and grey ramp generated by the host isolate the display stack.
Source content is variable by design. A photograph with a warm cast, a video with a colour grade or an application with an incorrect profile can make a neutral panel look wrong. The test is to remove the content: drive full white, full black, the three primary fields, a neutral grey ramp and a flat 50 percent grey from the host or a pattern generator. If the tint is present in every neutral field, it belongs to the display stack. If it appears only in one image, it belongs to the source or the colour pipeline.
Look at the pattern across the panel, not only at the centre. A uniform field that is yellow at the centre and neutral at the edges describes a different mechanism from a uniform field that is yellow everywhere. A grey ramp reveals gamma-related banding that a white field hides. A checkerboard can reveal crosstalk or mura that a flat field averages away. Record the pattern name and the drive level with each photograph.
The optical stack itself can shift colour through the cover glass, the adhesive, the polarizer and the backlight spectrum. Material data such as the Corning Gorilla Glass 3 product information describes the properties of that glass, not the colour performance of a finished module; use it to understand a material variable, not to set an acceptance limit.
Temperature history explains reversible and lasting shifts.
Cold panels shift colour, while sustained backlight heat can age the polarizer or LEDs; record panel temperature at observation and total operating hours.
Liquid crystal response and birefringence change with temperature, so a panel observed cold can show a colour and contrast difference that disappears at room temperature. That shift is reversible and should not be treated as aging. The opposite case is cumulative: heat from the backlight, absorbed sunlight or a hot enclosure can accelerate polarizer yellowing, adhesive hazing or LED output drift, and those changes persist after the unit cools.
Measure the panel temperature at the time of observation, not the ambient temperature alone. A thermocouple on the front stack or an infrared reading from a defined point is enough to distinguish a cold-start effect from a steady-state one. Record the warm-up time and the brightness setting, because both change the thermal load. For a field return, add the operating hours and the enclosure type; a sealed metal housing and an open frame produce very different internal temperatures.
If the discoloration changes with temperature but returns when the unit stabilizes, the finding is a thermal design issue rather than a panel defect. If it persists, the temperature history becomes evidence of accelerated aging and belongs in the RMA record.
Release the bezel and re-measure before blaming the panel.
If tint or mura changes when mounting pressure is removed, the cause is mechanical load in the assembly, and the fix belongs to the gasket or bezel.
A panel is a thin optical stack held between a cover glass and a backlight. A gasket that is too thick, a bezel that is not flat, a screw torqued unevenly or a connector that presses on the frame can deform the cell gap or the polarizer. The result is a local colour shift, a dark patch or a mura that looks like a panel defect but changes when the mounting load changes.
Remove the module from its enclosure, support it without pressure and re-measure the same points under the same lighting and drive pattern. If the discoloration fades or moves, the assembly is implicated. If it remains unchanged, the panel or the bonded stack is more likely to be the source. Photograph both states, because the comparison is the evidence.
Do not use finger pressure to test the effect. Local pressure can permanently deform the cell or the polarizer and convert a reversible assembly issue into a panel failure. Use the designed mounting points and a controlled release, and record the torque or compression that was present before removal. The optical bonding inspection guide describes the defect patterns that pressure and bonding faults produce.
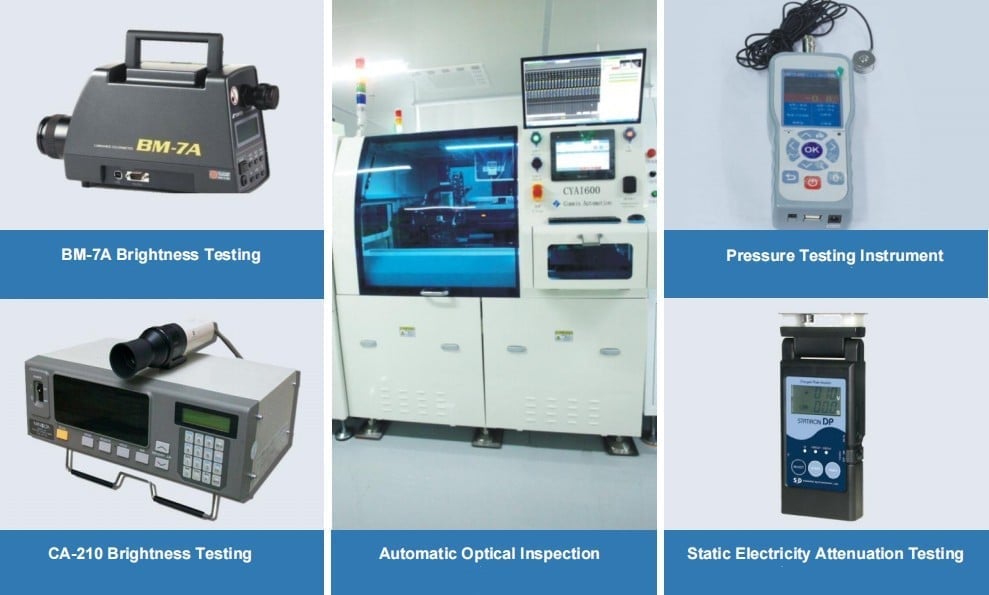
Measure luminance and white point at the same point.
Colour without luminance hides a dimming backlight; luminance without chromaticity hides a hue shift; report both at defined points after warm-up.
A colour meter reports chromaticity, and a photometer reports luminance; a colorimeter usually reports both, but only if the measurement is taken at the same point and under the same conditions. Report the white point as chromaticity coordinates and the luminance in cd/m², at the centre and at defined off-axis points. Include the instrument model, the aperture, the viewing geometry and the warm-up time. The SID ICDM display metrology standards are the entry point for the relevant measurement method, and the edition must be checked before quoting a procedure.
A dimming backlight and a hue shift can produce the same subjective complaint. If luminance has fallen while chromaticity is stable, the backlight or its drive is the likely cause. If chromaticity has moved while luminance is stable, the polarizer, the panel or the source profile is more likely. Measuring only one quantity leaves the two cases indistinguishable.
Report uncertainty with the reading. The NIST Technical Note 1297 describes how measurement uncertainty is expressed; it does not supply display acceptance thresholds. A difference smaller than the combined uncertainty of the instrument and the setup is not evidence of a change.
Use a retained reference when the change is gradual.
A golden sample or a baseline measurement from the same build proves that a panel changed; absolute targets vary by lot and cannot establish drift.
Absolute colour targets are useful for acceptance, but they cannot show that a particular unit has changed. Two panels from different lots can sit at different points within the same tolerance and still be compliant. To establish drift, compare the suspect unit with a retained sample of the same build, or with a measurement record taken when that unit was new. The comparison must use the same pattern, instrument, geometry and warm-up.
A golden sample is only useful if it has been stored under controlled conditions and its own history is known. A sample that has been left on a shelf in sunlight is not a reference. Record the storage location, the date and any prior measurements, and re-measure the reference at the same time as the suspect unit so instrument drift does not enter the comparison.
Where no physical reference exists, a baseline measurement from the production record can serve the same purpose. That is one reason to keep optical measurements with the module serial. The CIE Colorimetry publication defines the colorimetric framework; the measurement procedure still has to come from the applicable display metrology standard.
Destructive analysis comes after non-destructive evidence.
Reserve cross-sections or material tests for cases where non-destructive evidence cannot separate aging, contamination and mechanical damage, and the answer changes a design.
Destructive analysis destroys the unit that carries the evidence. It is justified when the non-destructive record has narrowed the cause to two or three mechanisms that cannot be separated without looking inside, and when the answer will change a design, a supplier or a process. It is not justified as a first step to satisfy curiosity, and it is rarely justified on the only returned unit.
Typical targets are the polarizer-to-glass interface, the adhesive edge, the seal and the LED emission surface. A cross-section can show delamination, contamination or voiding; a peel test can show adhesion strength; a spectral measurement of the backlight can separate LED aging from a colour-filter shift. Each test needs its own sample and its own record, and the result should be tied back to the non-destructive measurements.
Plan the destructive work before cutting. Photograph and measure the intact unit first, keep a sister sample where possible, and record the exact location of the section. A result that cannot be located on the original panel is difficult to use in a supplier discussion.
Send serial, build, measurements and controlled photographs.
An RMA package needs the serial and build, test pattern, instrument and warm-up, measured points, controlled photographs with a neutral reference, and service history.
The package should let the supplier reproduce the observation without the physical unit. Include the module part number, build revision and serial; the test pattern and drive level; the instrument model, aperture and warm-up; the measured points and values with uncertainty; the ambient and panel temperature; the mounting arrangement; and the time in service. Add controlled photographs with a neutral reference and fixed exposure, and state whether the unit was re-measured after the bezel was released.
The table below is a structure for that record. It is not a set of limits; the acceptance owner decides which values apply to a given product.
| Test pattern or point | Viewing geometry | Instrument and warm-up | Raw reading or uncertainty | Acceptance owner |
|---|---|---|---|---|
| Full white, centre | Normal to panel, 50 cm | Colorimeter, 30 min warm-up | Luminance and chromaticity with uncertainty | Product specification |
| Full white, corners | Normal to panel, same distance | Same instrument and aperture | Point-by-point values | Panel drawing |
| 50% grey ramp | Normal to panel | Same instrument | Gamma and banding observation | Display requirement |
| Off-axis white | 30° and 60° from normal | Same instrument, geometry recorded | Chromaticity shift | Application requirement |
| After bezel release | Same as baseline | Same instrument and warm-up | Change against baseline | Mechanical design owner |
Keep the raw files and the measurement log with the RMA number. A summarized value without the setup cannot be checked, and a photograph without a neutral reference cannot be compared. Where the product is a medical display, a defined grayscale response measurement may also be required; the DICOM PS3.14 chapter describes measurement of grayscale standard display function agreement and is not a certification of the device.
Can source-image color settings imitate a hardware discoloration fault?
Yes. A wrong colour profile, an application-level tint or a compressed test image can make a correctly performing panel look yellow or green. Generate a neutral full-field pattern and a grey ramp from the host, bypass the image pipeline where possible, and compare the same pattern on a known-good module before ordering a hardware investigation.
Should photographs include a neutral reference and fixed exposure?
They should. Auto white balance, auto exposure and a coloured background can create or hide a tint. Photograph the module with a neutral grey card in the frame, fixed exposure and white balance, the same light source and the same distance for every unit, and keep the raw file so the comparison can be repeated.
Does replacing a backlight establish that the LCD cell was healthy?
No. A new backlight changes the illumination spectrum and can make a cell or polarizer problem less visible without removing it. If the backlight is replaced during diagnosis, re-measure the white point and luminance at the same points and record the replacement, so a later recurrence is not attributed to the original panel.
What is LCD bruising?
Bruising is a local discoloration or mura caused by mechanical pressure on the panel stack, often from a bezel, gasket or handling. It may fade when the pressure is removed or may persist if the cell or polarizer has been permanently deformed. Release the mounting load and re-measure before deciding whether the panel itself is defective.
If a discoloration claim needs a measurement record before a supplier discussion, send the module serial, test patterns and instrument data to the CDTech engineering team. The team can compare the report with the module’s build and inspection data and identify which layer needs further evidence.
By continuing to use the site you agree to our privacy policy Terms and Conditions.